
AI Summary
Producing flexible wash basin and sink waste pipes on a Single Wall Plastic Corrugator Machine (SWC Extrusion Plant) follows a clear procedure: record the installation layout, fix the corrugated profile, complete material preparation and pre start checks, run trial production, plan cut lengths, confirm connector fit, check leakage and drainage, and shut down safely. Each stage carries its own precautions.
Procedure Overview for Flexible Wash Basin and Sink Waste Pipes
A Single Wall Plastic Corrugator Machine (SWC Extrusion Plant) produces the corrugated body used in a flexible waste pipe for wash basins and sinks. When planning a wash basin pipe making machine, manufacturers should define the pipe profile, cut length and connector interfaces for the intended corrugated sink drain pipe assembly. Sanitary pipe manufacturing also requires checks that the completed assembly drains correctly and remains leak free under its specified service conditions.
Keep three scopes separate throughout:
- Corrugated pipe: the single wall body, with its profile, material and length.
- Connector interfaces: end fittings or adaptors joining the pipe to outlet and drain.
- Drainage assembly: pipe, connectors and seals working together when installed.
Volcano Flexi Tech Industries states that its SWC line makes the corrugated body of these pipes, with threaded connectors fitted afterwards. This guide does not replace the machine manual or a plumbing installation guide.
Routing Procedure for Under Basin Flexible Waste Pipes
The first step is recording the installation envelope the pipe must serve.
Procedure
- Record the relative positions of the outlet and drainage connection, including offset and height difference.
- Note cabinet walls, supports and other obstructions along the route.
- Confirm space for the pipe route and for hands and tools during assembly.
- Confirm access for fitting, inspection and servicing.
Precautions
- Do not treat flexibility as a substitute for a suitable drainage route.
- Avoid routes with sharp bends, water holding sags, or compressed or overstretched sections.
- Follow the target market’s plumbing guidance rather than assumptions about what a flexible pipe tolerates.

Flexibility Precautions for Corrugated Sink Drain Pipe Profiles
The profile must let the pipe bend along the intended route while keeping a clear bore. According to Volcano Flexi Tech Industries, the profile for basin and sink waste pipe is chosen so the pipe bends easily under the basin yet still holds its shape.
Procedure
- Define the bends required by the intended layouts.
- Evaluate resistance to kinking or local collapse on samples bent to those routes.
- Check corrugation uniformity along the length.
- Confirm the pipe holds its routed position under intended assembly conditions.
- Confirm the polymer grade and mould profile suit the design.
Precautions
- Never assume kink resistance; verify it on samples.
- Do not describe the pipe as extendable, telescopic or suitable for repeated adjustment unless verified for that purpose.
Material Preparation and Pre Start Checks for the SWC Extrusion Plant
Pre start checks confirm that material, tooling and utilities match the approved pipe before the line runs.
Procedure
- Confirm the approved material grade and record its batch.
- Keep feed material, hoppers and handling containers clean and free of contamination.
- Condition material where the supplier or manual requires it; Volcano Flexi Tech Industries notes that polyamide granules need drying before extrusion.
- Verify that the fitted die and mould blocks match the approved drawing. Volcano Flexi Tech Industries designs its SWC plant for easy mould block changes, so check the set every time.
- Confirm cooling readiness, including chilled water to the corrugator’s inbuilt cooling channel and the air chiller.
- Complete every pre start check prescribed in the machine manual, including lubrication and control panel readiness.
Precautions
- Do not start with an unidentified or mixed material batch.
- Never skip a manual check or remove a guard.
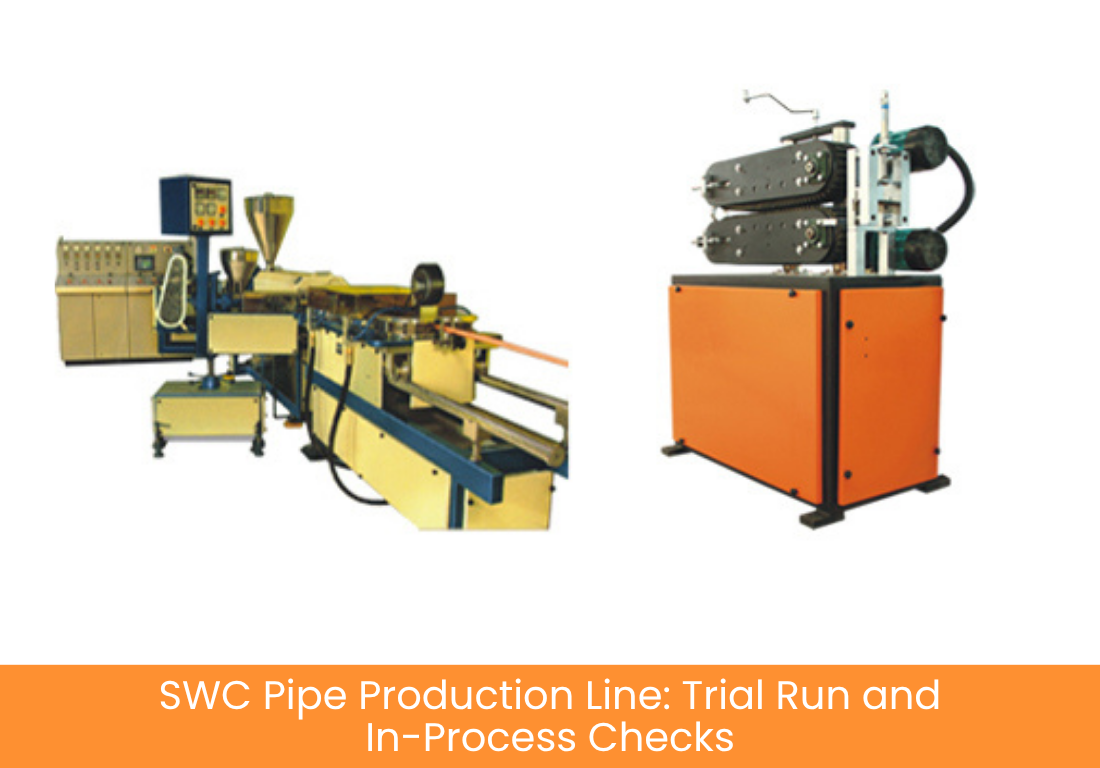
Trial Production and In Process Precautions on the SWC Pipe Production Line
Trial production confirms that the line makes the approved pipe consistently before release.
Procedure
- Coordinate extruder output with corrugator speed through the control panel, which uses AC drives and temperature controllers to synchronise the line.
- Check cooling performance and puller settings; the Volcano puller has adjustable roller gap and belt tension for different pipe sizes.
- Inspect first samples against the drawing for profile, dimensions and surface condition.
- Verify that cut ends have the position and finish the connector requires.
- Segregate and label defective lengths so they cannot reach packing.
- Record approved settings and observations for repeat runs.
Precautions
- Take settings from validated trials and the manual, not general guidance.
- Treat moving belts, mould blocks, the cutter and heated equipment as hazards, and never adjust around moving components outside the approved procedure.
- Know the location of the emergency stop arrangement before running.
Cut Length Procedure for Flexible Waste Pipe Assemblies
Procedure
- Define the intended installed reach along the route.
- Add connector engagement allowances at each end.
- Set the pipe variants offered for different layouts.
- Agree the measurement condition: relaxed, straightened or another defined state.
- Specify the cut position on the profile and the end finish needed for fitting.
For cutting, Volcano Flexi Tech Industries offers a pneumatic cutter triggered by the panel electronics and modular corrugators with 2000, 2500 or 3000 mm chain lengths matched to pipe piece length. Confirm the cutting configuration during the enquiry.
- Label manufactured cut length, installed reach and any approved adjustable length separately.
- Take tolerances from the approved pipe specification, never from assumption.
Connector Fitting Procedure after the Wash Basin Pipe Making Machine
Procedure
- Match pipe outside diameter, profile and cut position to the selected connector.
- Confirm whether the interface is threaded, push fit or another approved design, and which drawing governs it.
- Specify seal type and position where seals form part of the approved assembly.
- Check that the connector seats correctly and stays secure.
- Record whether connectors are supplied separately, and by whom.
Precautions
- Do not assume different profiles accept the same connector.
- Use adhesives, clamps or sealing methods only where a specification calls for them.
Leakage and Drainage Check Procedure in Sanitary Pipe Manufacturing
Pipe inspection confirms dimensions and profile, while assembly evaluation confirms that pipe, connectors and seals perform together. A corrugated sink drain pipe can pass dimensional checks yet leak at a poorly matched joint.
Procedure
- Check for leakage through the pipe wall and at each connection point.
- Check drainage through the intended route, not only with the pipe straight.
- Look for flow restrictions from deformation, kinking or unsuitable assembly.
- Apply the service conditions set in the pipe specification.
- Record the configuration: pipe batch, connectors, seals and route.
Precautions
- Do not assume a pressure test suits every gravity waste assembly; take methods and acceptance limits from the applicable specification.
- Do not treat one successful assembly as proof of compatibility with every connector or layout.

Shutdown and Changeover Precautions for the Single Wall Plastic Corrugator Machine
Shutdown and mould changes carry their own risks.
Procedure
- Follow the manufacturer’s shutdown sequence in the machine manual.
- Isolate energy using the prescribed procedure before any tooling access or cleaning.
- Identify and label remaining material and partly finished pipe.
- Record the mould set now fitted and the next set planned.
Precautions
- Do not access tooling until energy isolation is confirmed.
- Allow for heated equipment and use the safe access procedure during changeover.
- Refit all guards before restarting.
About Volcano Flexi Tech Industries
Volcano Flexi Tech Industries manufactures corrugated pipe machinery in Ahmedabad, Gujarat. Its range covers single wall corrugator machines, double wall corrugator machines including a 500 mm ID model for sewage drainage, and plastic extrusion machinery such as pipe, profile, granulation and wire and cable plants. Among these, the SWC lines make the corrugated body of basin and sink waste pipes.
Conclusion on Safe SWC Waste Pipe Production
Safe, repeatable production of flexible wash basin and sink waste pipes depends on following each procedure stage and its precautions, from layout capture to assembly checks. Manufacturers planning this production are welcome to discuss their intended pipe design and the relevant SWC configuration with Volcano Flexi Tech Industries.